Built Different.
From The Inside Out.
Accuracy begins with the bore. Before a barrel is chambered, threaded or profiled, its internal geometry has already established the foundation for how it will perform.
Control The Process That Creates The Barrel.
MNKY Barrels was built around precision manufacturing. The process focuses on bore geometry, rifling consistency, stress management, machining, chrome lining and dimensional inspection.
Rather than treating inspection as a final checkpoint, dimensional control is integrated throughout manufacturing.
From Raw Material
To Final Acceptance.
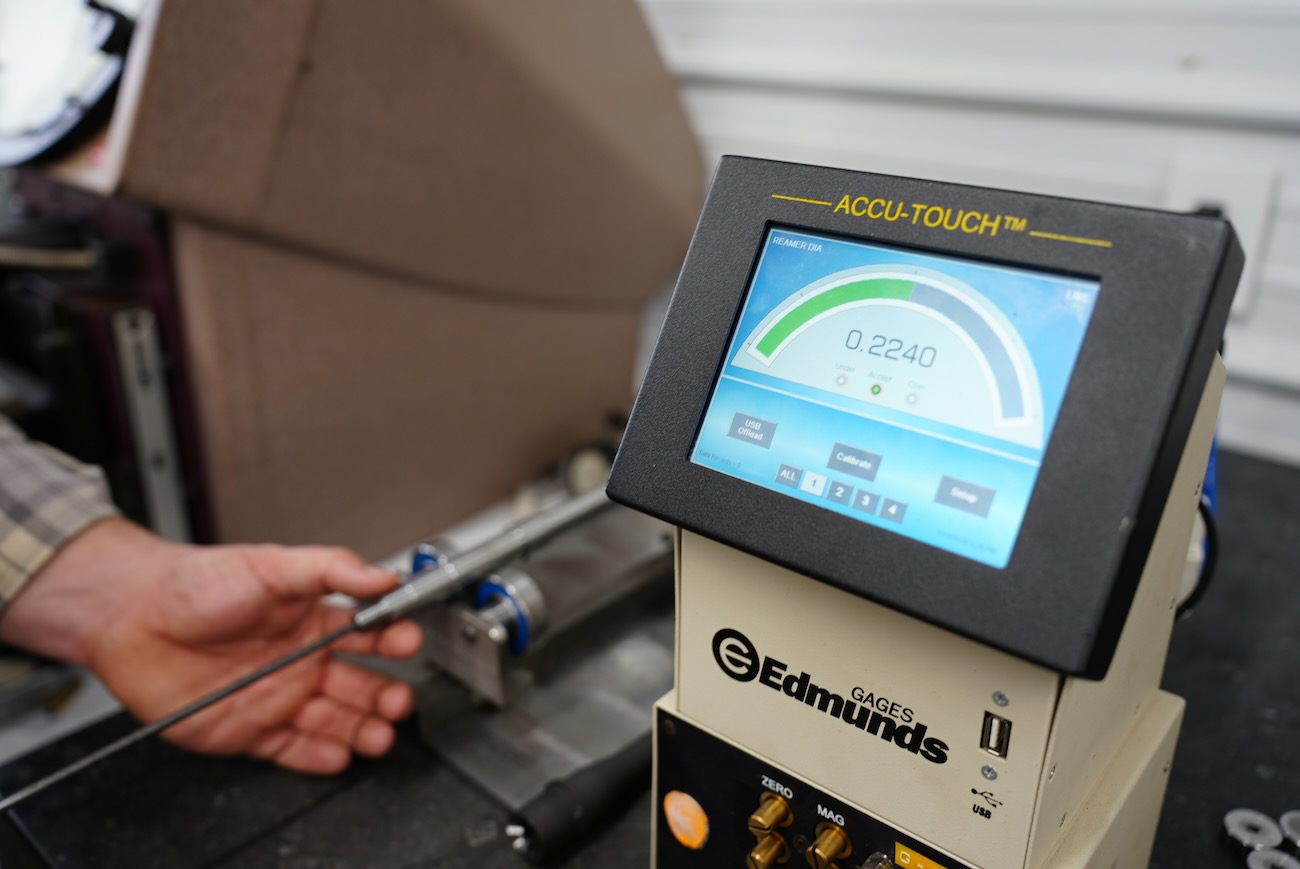
Dimensional inspection is not a single checkpoint. Every barrel is air gauged before rifling and again after rifling. Air Gauged Match Grade barrels receive an additional dimensional qualification after chrome lining.
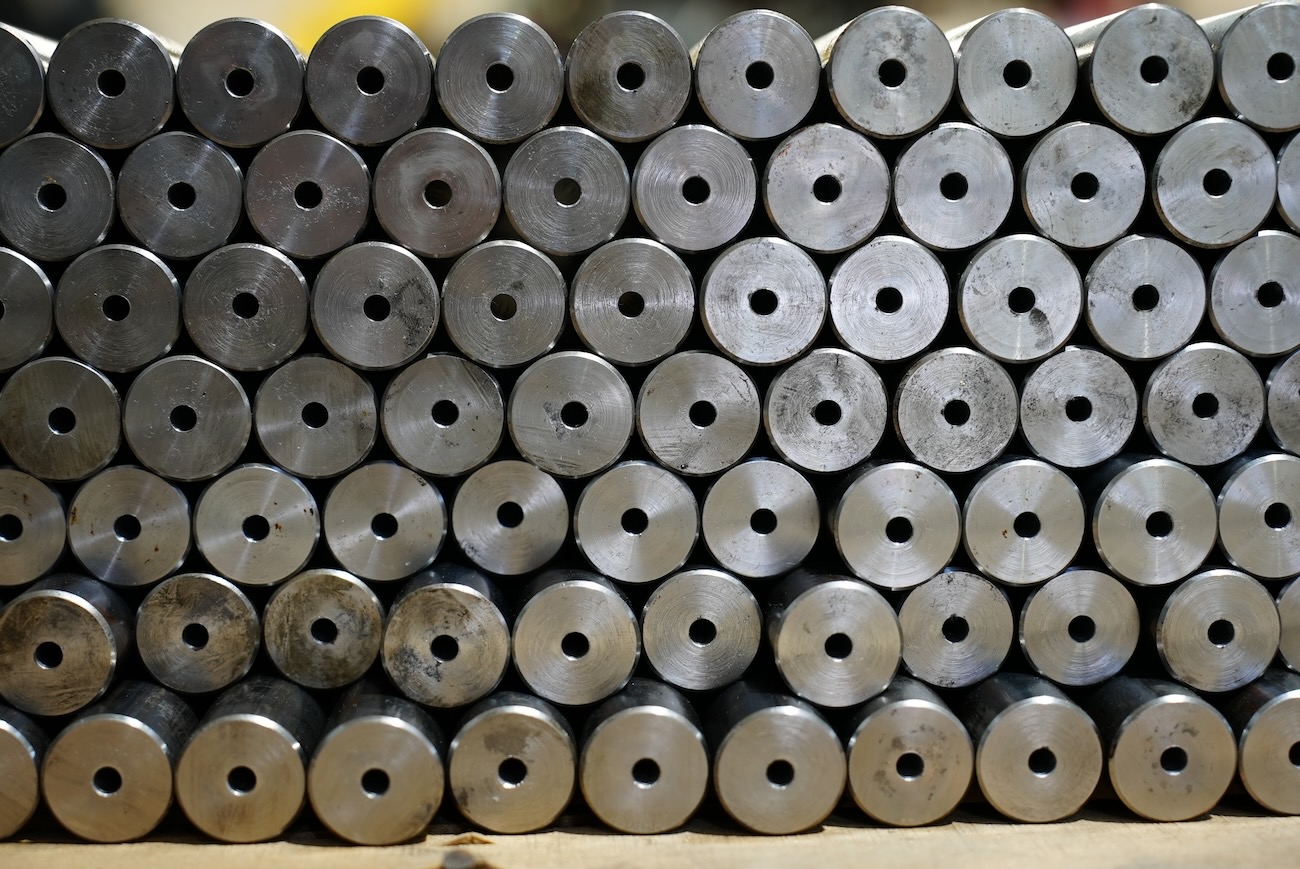
Deep-Hole Drilling
The bore begins with precision deep-hole drilling to establish a straight and consistent foundation.
Precision Reaming
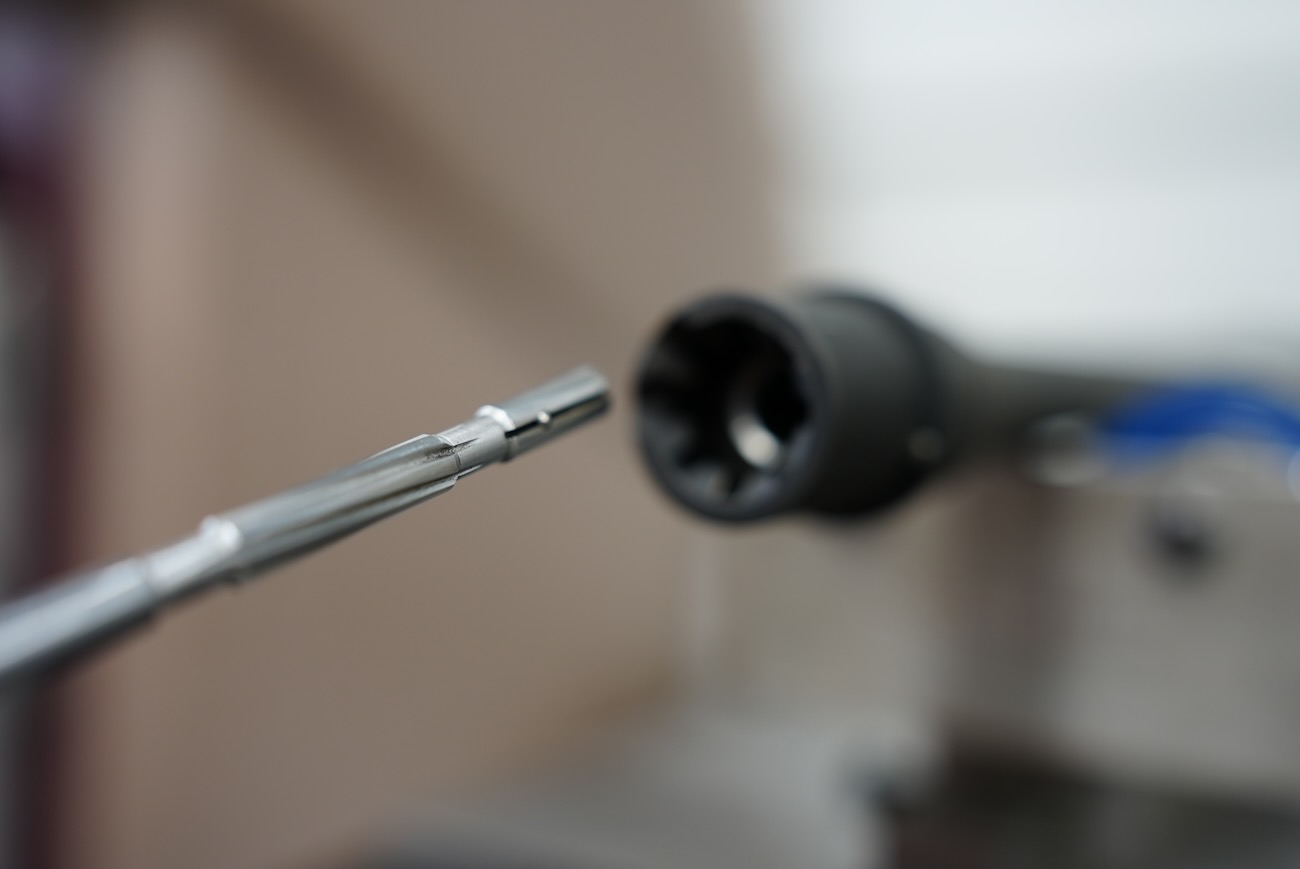
Bores are reamed to improve internal geometry and surface finish.
Honing
Bores are honed using a proprietary machine to further refine surface finish.
Initial Air-Gauge Inspection
Critical internal dimensions are measured before rifling to establish a dimensional baseline.
Precision Rifling
The rifling process is controlled to produce consistent lands and grooves while maintaining dimensional uniformity.
Post-Rifling Air-Gauge Inspection
Every barrel is air gauged again after rifling to verify bore and groove dimensions following the rifling operation.
Stress Relief
Barrels undergo a controlled stress-relief process to reduce internal stresses introduced during manufacturing.
Hand Lapping
Following stress relief, barrels are hand lapped to further refine the internal finish.
CNC Machining
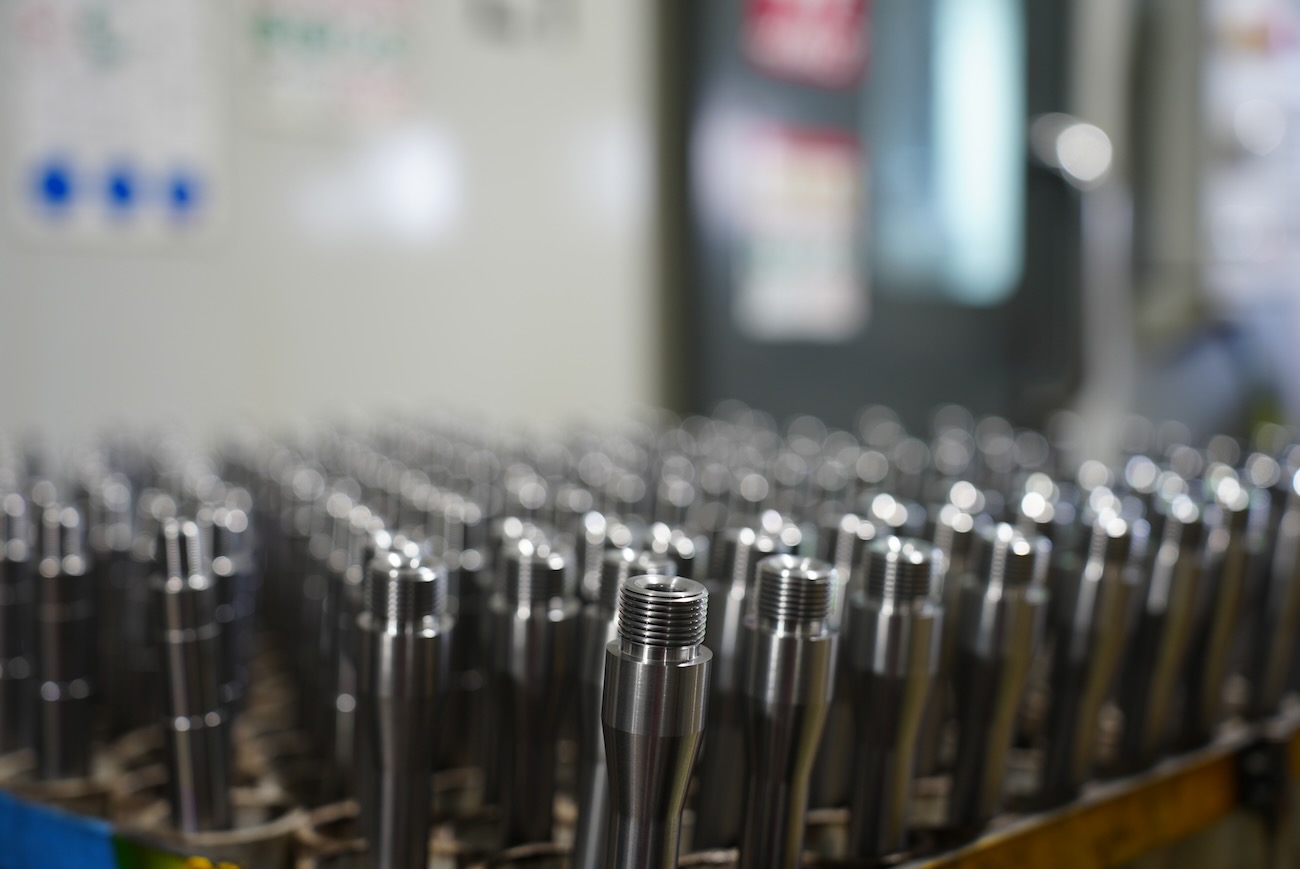
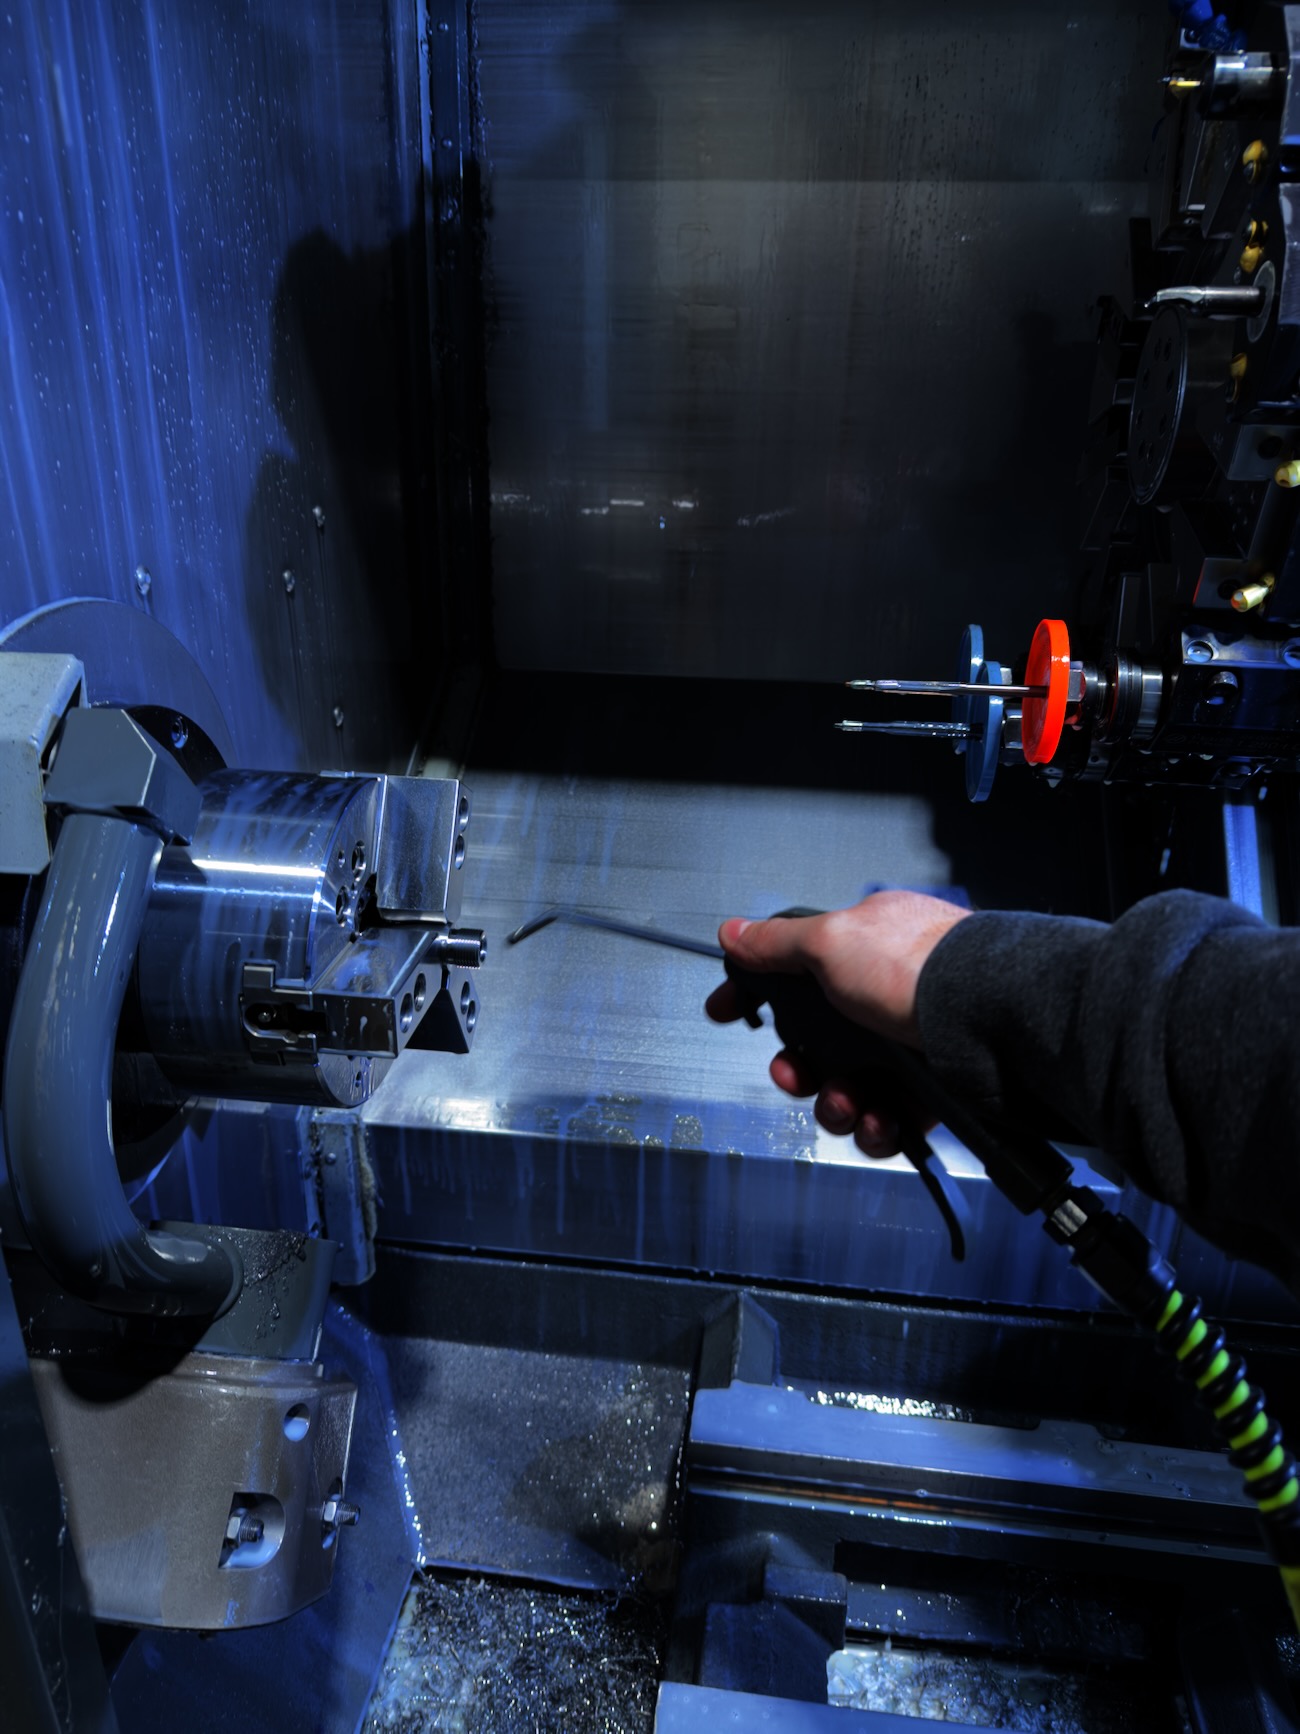
Chambers, profiles, threads, gas features and other external geometry are precision machined.
Chrome Lining
The bore and chamber are chrome lined for wear, heat and corrosion resistance while maintaining dimensional control.
Final Air-Gauge Qualification
Air Gauged Match Grade barrels are inspected again after chrome lining for final dimensional qualification and selection.
HP / MP Testing
Every MNKY barrel is high-pressure proof tested and magnetic-particle inspected before final acceptance.
Build The Bore Correctly First.
The manufacturing story begins inside the barrel. Bore quality and dimensional consistency are the foundation for every operation that follows.